
What Are the Methods for Repairing Scratches on Hydraulic Cylinder Piston Rods?
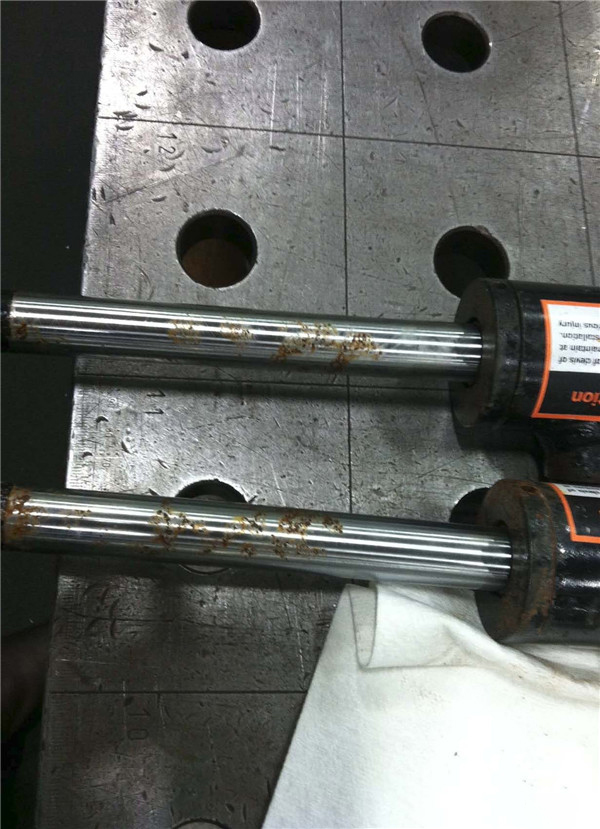
The cylinder of large forging equipment is prone to scratches and damage on the surface of the Cylinder Piston Rod, resulting in oil leakage, reduced pressing accuracy, and even debris contaminating the entire hydraulic system.
Because it is a large forging equipment, disassembling the cylinder is a very labor-intensive and time-consuming task. In addition, problems such as cylinder scratches are difficult to repair quickly. In response to this frequent problem, equipment maintenance personnel have tried every possible way to repair some of these faults in combination with their own maintenance conditions and strength. After the repair, they can basically meet the operating requirements.
However, for super-large plunger cylinders or cylinders with serious scratches and damage, our own maintenance force seems to be unable to cope with it, and we can only rely on professional maintenance companies to solve it.
Combining our own maintenance methods and consulting some repair methods of professional companies, this paper briefly summarizes the repair methods for the surface damage of the Hydraulic Cylinder Piston Rod (plunger), hoping to bring you some help!
According to the piston size requirements, there are two main methods: size recovery repair method and size reduction repair method. The main implementation methods are machining, welding (surfacing, repair welding, brazing, etc.) and electroplating (low-temperature iron plating, chrome plating), polymer composite material spraying, etc.
1. Size restoration repair method
1.1. For local rust on the piston rod, if the area is not large, not concentrated, and the number is small, stainless steel argon arc welding is used to repair the rusted parts by local welding, grinding, polishing, etc. This method is simple and low-cost. And it can meet the use requirements.
1.2. For piston rods with local coating shedding, shallow rust pits, large areas, etc., the chrome layer is removed, polished, and re-chrome plated. The tolerance requirements must be guaranteed after electroplating. If the plating pits of some parts are deep after polishing, brazing can be used for local welding, manual grinding, chrome plating after repair, hard chrome plating (plating thickness 0.03~0.05mm) and polishing. When repairing manually, it is best to process a grinding sleeve according to the outer diameter of the piston rod, grind the local repair part, and make its surface roughness reach Ra 0.1~0.2μm (although this is difficult).
1.3. If the piston rod is seriously corroded and cannot meet the electroplating requirements after chrome removal and polishing, the piston rod should be straightened and ground and turned. When the grinding size is less than 0.5mm of the original size and can meet the electroplating requirements, it can be treated by copper plating first and then chrome plating. To meet the use requirements.
If this method still cannot meet the requirements, the original size should be directly turned down by 4-5mm, and then thermal spraying or iron plating methods should be used to restore the original size and then grind and repair with chrome plating. This method is costly and expensive. Moreover, after iron plating and chrome plating, the chromium layer is easy to fall off, and the spraying quality is difficult to control.
1.4. At present, some high-performance polymer composite materials are also used to repair minor scratches on the piston. The high-performance epoxy two-component composite material reinforced by nano-inorganic materials can adhere well to the piston surface, has good high temperature resistance and chemical corrosion resistance, can be quickly machined after spraying, has simple technical operation, high repair quality, saves time, and is low cost. However, for high-pressure cylinders and fast and frequent reversing cylinders, the spray coating may fall off under pressure shock, so use it according to the working conditions.
2. Reduction size repair method
For pistons with severe corrosion and scratches on the surface, it can also be repaired by directly reducing the size. Generally, the piston rod is corrected, turned, and ground when the diameter is reduced. When it is 5mm smaller than the original nominal size, it can meet the electroplating requirements, and the repair cost is low, which can meet the use requirements.
The piston rod is reduced by 5mm. Generally, in the standard series of cylinder piston rods, the seal can also use a standard seal ring. If this method is used for repair, the piston sleeve needs to be redesigned and manufactured, and the corresponding seal is selected for assembly. (Remember: Be sure to keep the data in the equipment file for future maintenance)
Summary
The piston rod of the hydraulic cylinder of large forging equipment is prone to scratches and damage, which leads to problems such as oil leakage, reduced pressing accuracy, and hydraulic system pollution. Since the equipment is difficult to disassemble and the maintenance is time-consuming and laborious, this article combines its own maintenance methods and the maintenance methods of professional companies to summarize the repair methods of piston rod surface damage. There are mainly size recovery repair method and size reduction repair method. The size recovery method includes argon arc welding repair for local rust spots, de-chrome re-plating of coating shedding and rust pits, lathing and electroplating treatment for severe corrosion, and the use of high-performance polymer composite materials to repair minor scratches. The size reduction repair method is to reduce the diameter of the severely corroded and scratched piston rod by 5mm, and meet the electroplating requirements after correction, lathing, and grinding. This method requires the redesign and manufacture of the piston sleeve and the selection of corresponding seals. The maintenance cost is low and can meet the use requirements.